In short
PCB assembly traceability connects a physical board or batch to the design revision and manufacturing history behind it. Depending on the project, that can include component lots, a unit or panel identifier, inspection and test results, and the changes made during production. Decide the required level of detail and retrieval needs before the build so the record answers a real product question.
For repeatable pilot and small-batch orders, review the files, sourcing and schedule on the low-volume PCB assembly page.
PCB assembly traceability makes it possible to work backward from a board or batch to the files, materials and production steps used to build it. A barcode helps identify the unit, but its value comes from the revision, lot and process information linked to that identifier. The right level of tracking depends on the product and what a later quality question needs to establish.
Use the lot, revision and quality-record controls here alongside quality control, PCB assembly and component sourcing. For a prototype moving into repeat production, use the prototype-to-production checklist alongside this record baseline.
Give each PCBA build a clear identity
Before a record can be trusted, the team must know what it belongs to. Identify the assembly part number, revision, variant or configuration, BOM and approved alternate status, fabrication and assembly data, build stage and acceptance requirements. Resolve conflicting filenames or unapproved edits before production release; a detailed lot history cannot repair an uncertain baseline.
| Record layer | Question it answers | Example project decision |
|---|---|---|
| Released configuration | Which files, BOM, variant and instructions controlled this build? | Freeze a revision and name the approval authority for changes. |
| Material identity and lots | Which specified material, component or lot is linked to the agreed build scope? | Define which parts require lot linkage and who supplies the source data. |
| Product or panel identifier | Which physical unit, panel or batch does a record describe? | Agree identifier format, placement and the level at which it is applied. |
| Process and inspection evidence | What route, checks and dispositions applied to the released build? | Specify the selected evidence, not every possible factory record. |
| Electrical or functional evidence | Which defined test result belongs to this build? | State program, limits, result format and failure authority when testing is in scope. |
| Retention and retrieval | Who keeps the agreed record and for how long? | Put retention, access and handover responsibilities in the project agreement. |
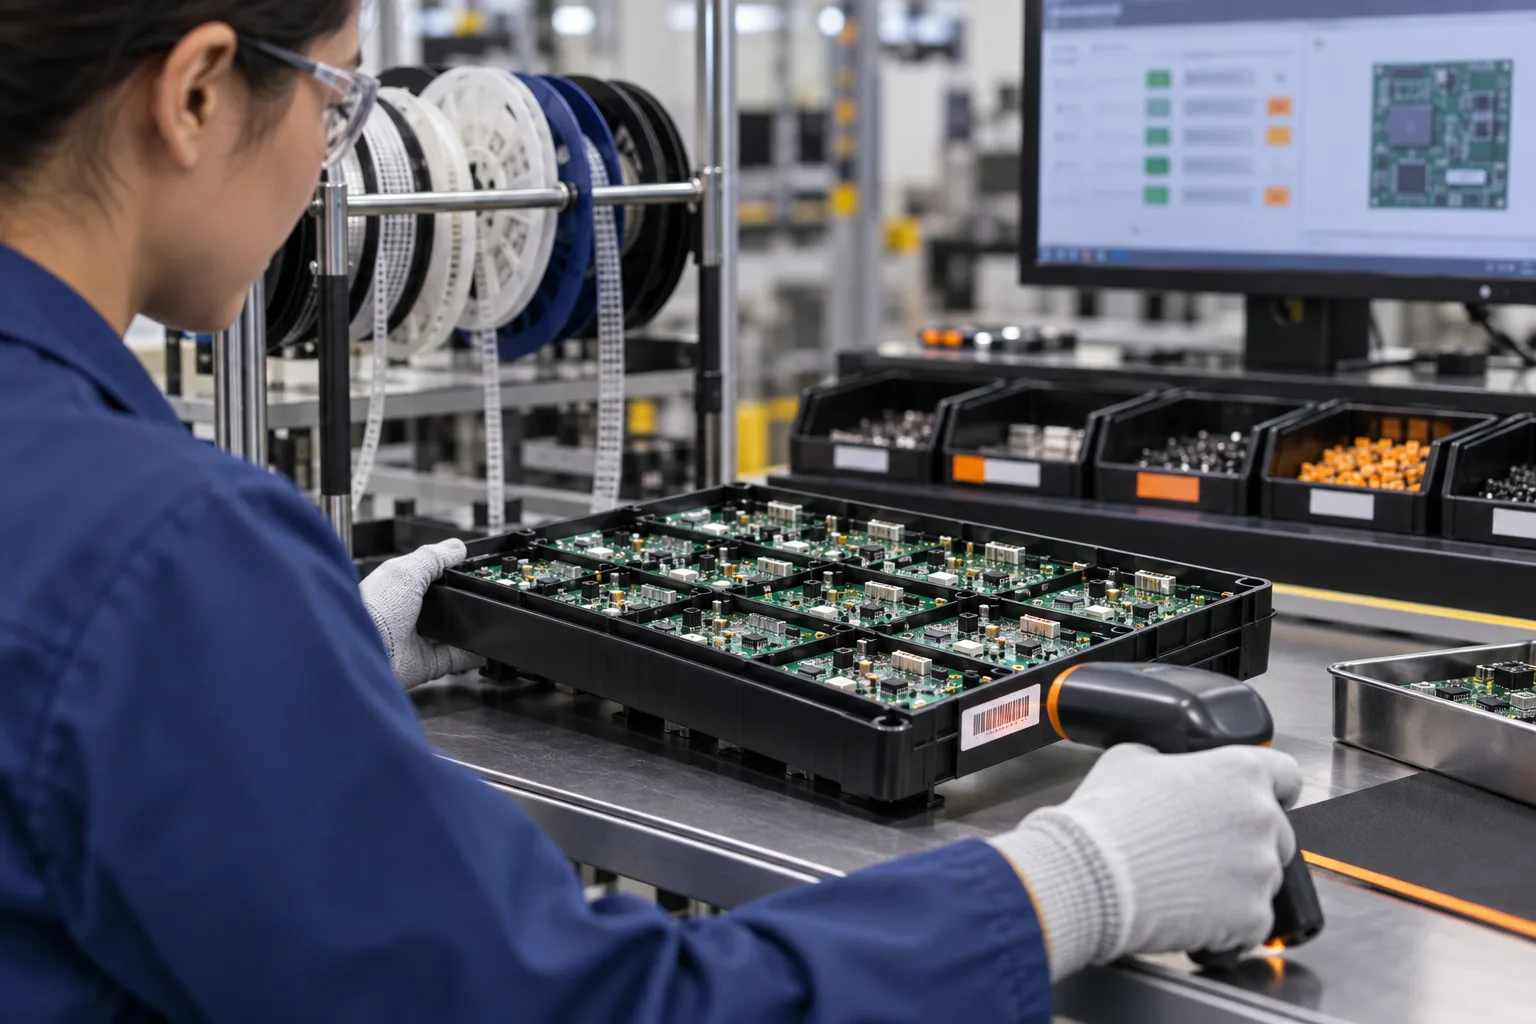
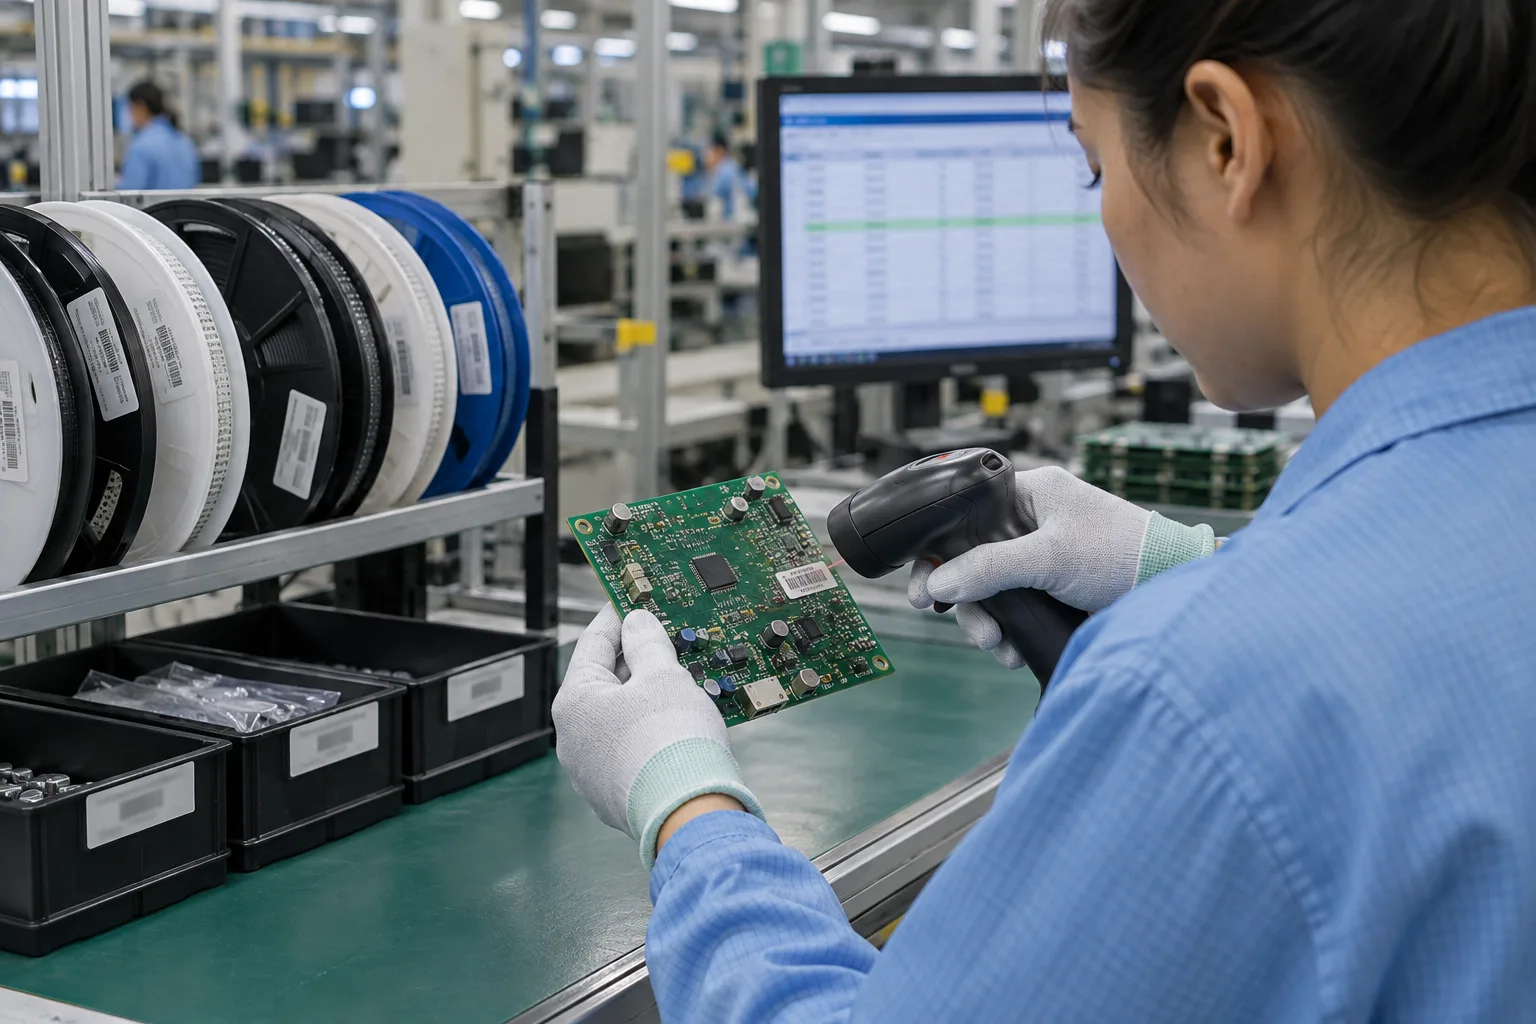
AI-generated illustration: Operator scanning a PCBA lot at an assembly workstation.
Choose the right level of lot and unit tracking
The public scope of IPC-1782 frames traceability as a risk-based topic. That is a useful buyer principle: start with the product, failure-containment and contractual question, then define the evidence proportional to it. A simple prototype, a controlled medical or industrial program, and a build with customer-consigned material may require different identifiers, source evidence, retention and retrieval paths.
Do not assume that every order includes serial-level traceability, every component lot, a fixed archive period or a regulatory record package. Those items must be requested, reviewed for feasibility and captured in the agreed manufacturing and documentation scope. The same applies to supplier data: an invoice, distributor label or incoming record may not answer the same question as a unit-level material link.
Link materials, process steps and test results
A practical baseline assigns an owner to each link. The customer or product owner normally controls released product requirements and change approvals. The assembly route controls how project-agreed identifiers and records are captured. The sourcing route identifies who supplies material documentation, who may approve alternates and how consigned-material boundaries are handled. Quality and engineering need a defined failure disposition path.
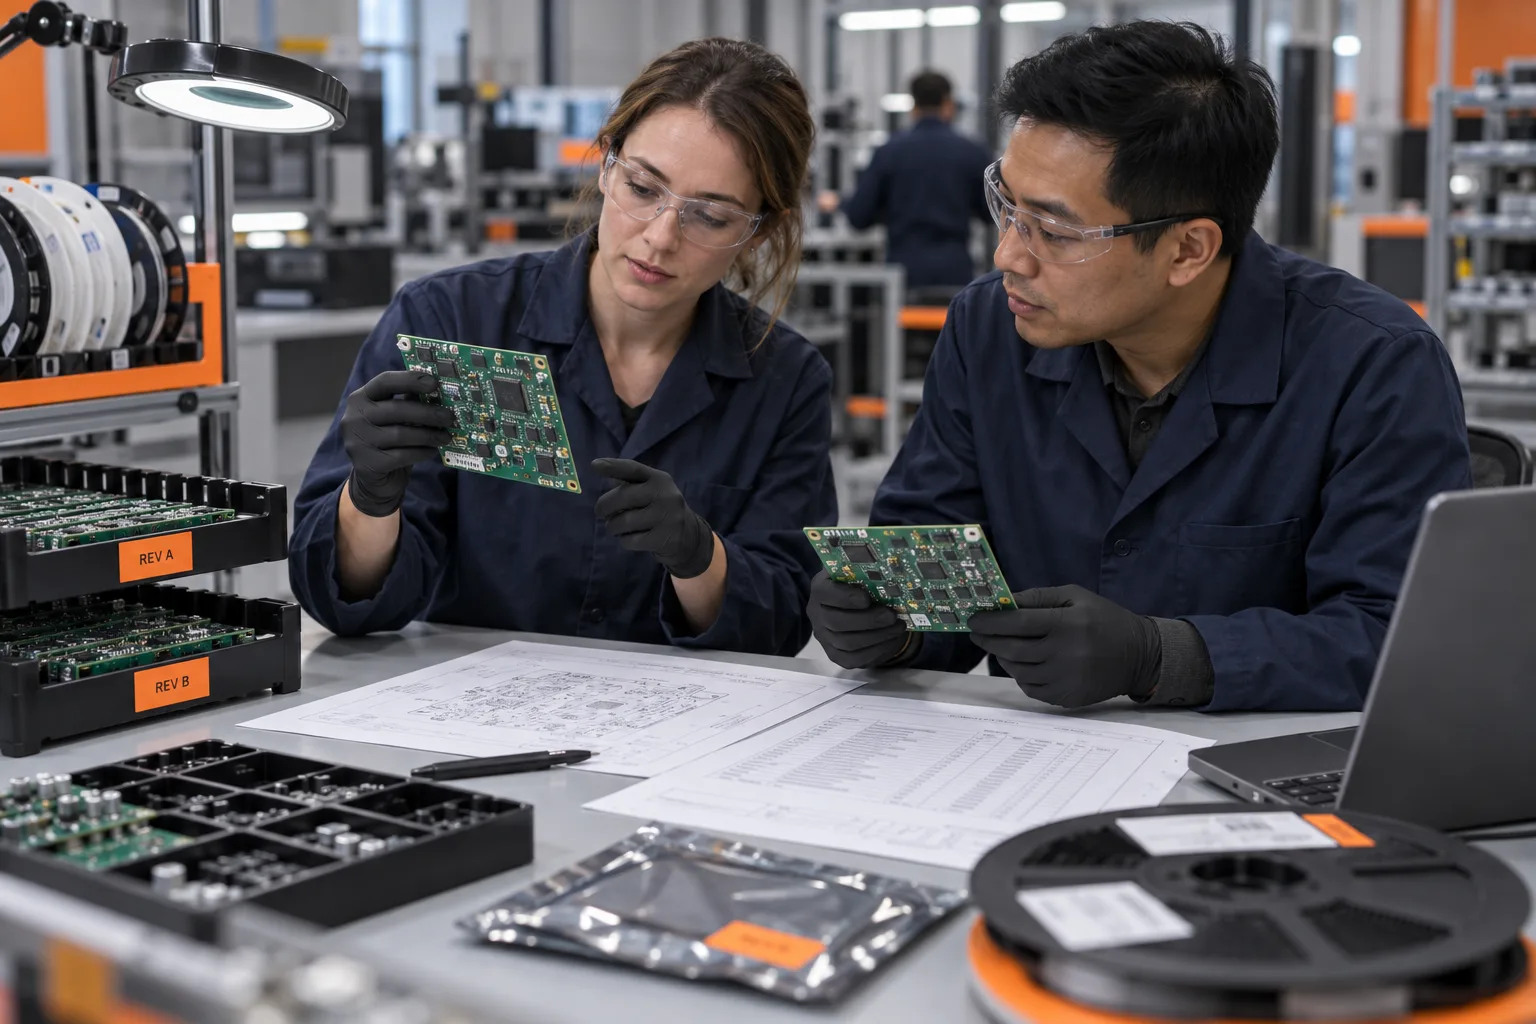
AI-generated illustration: Engineers comparing two PCBA revisions and build materials.
PCB assembly traceability checklist
- Which part number, revision, variant and file manifest are controlling?
- Which materials, lots, labels or source records must be linked, and at what level?
- What identifier applies to a unit, panel, batch or shipment?
- Which process, inspection, X-ray, electrical or functional records are required for this build?
- What result format, failure disposition and change approval path apply?
- Who owns retention, retrieval, access and handover of the agreed record set?
- What change reopens the baseline: BOM, alternate, firmware, process, test, supplier or acceptance requirement?
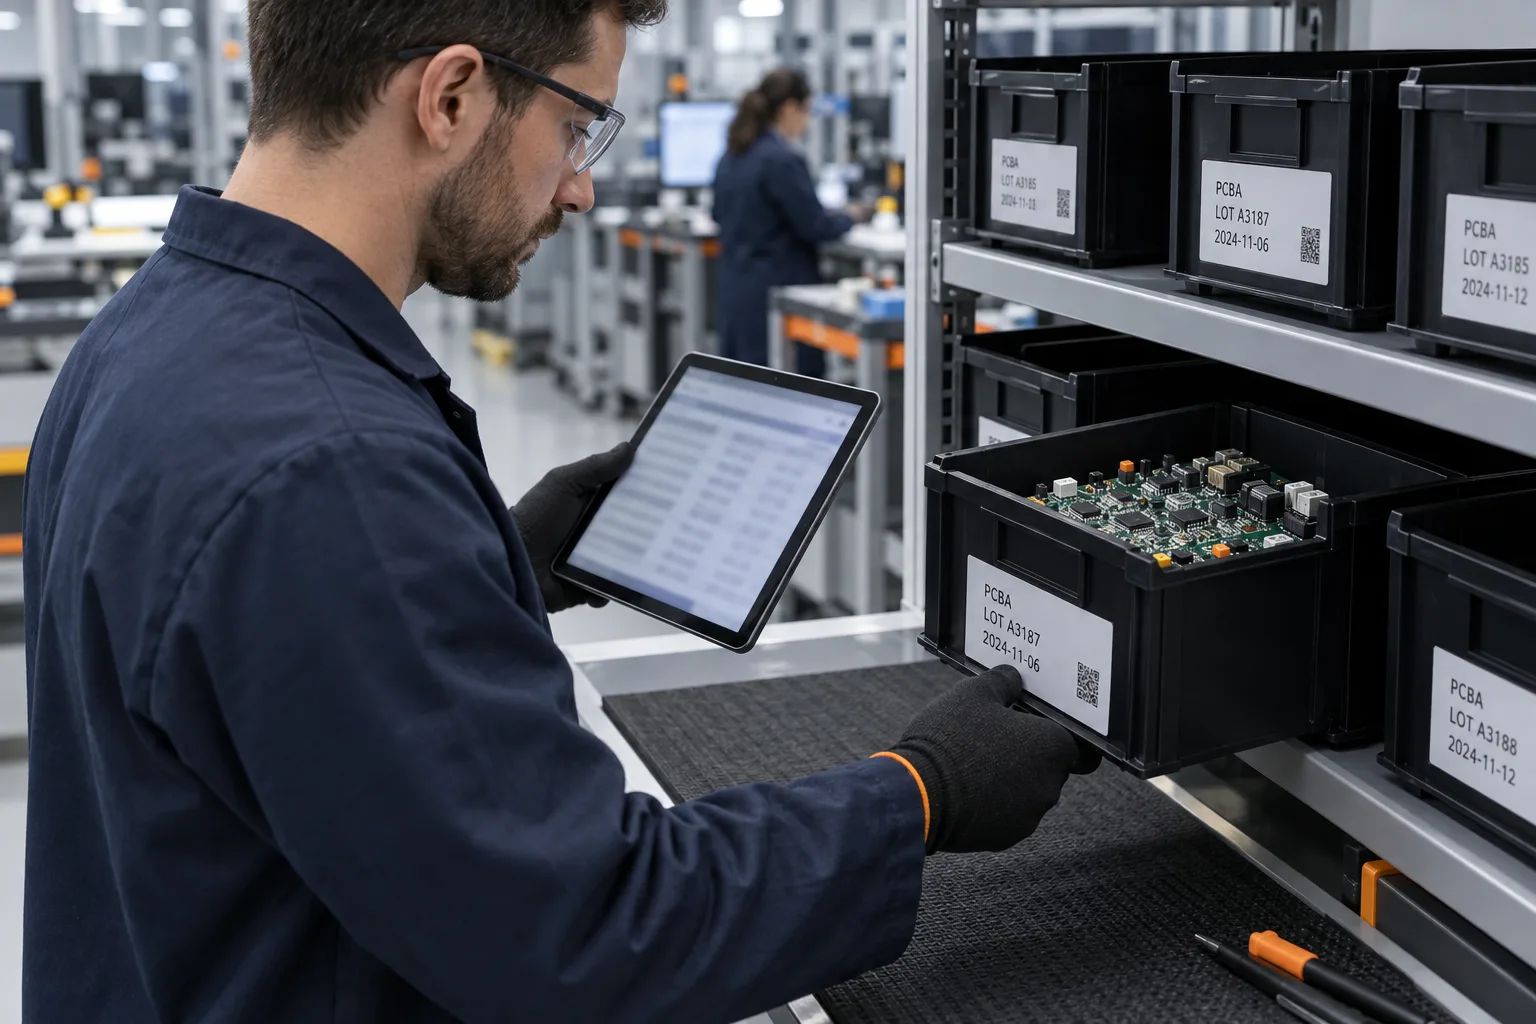
AI-generated illustration: Engineer retrieving a PCBA lot and its manufacturing history.
Connect inspection and test results to the right board
A record is useful only when it identifies what was observed and under which approved conditions. For hidden-joint evidence, the BGA X-ray guide explains why package, image method, criteria and scope matter. For electrical evidence, define the test access, program, limits and result format through PCB assembly testing. A passing result supports only the check performed; it should not be re-described as proof of unrelated conditions.
What to ask for in a traceability quotation
Provide the released file package, BOM and alternate rules, quantity and build stage, material sourcing model, required identifiers, selected evidence records, intended recipient and retention or retrieval expectations. PCBArise can use those inputs to discuss a project-specific route through a quote review. The quotation and approved documentation scope—not this guide—define the records supplied for the order.
FAQ
Common questions
What is PCB assembly traceability?+
It is the controlled link between a released PCBA build identity and the agreed material, process, inspection, test and disposition records needed to answer later quality or change questions.
Does traceability require serialization on every order?+
No. Serialization, unit identifiers, panel identifiers and lot-level records should be selected from the project risk, contract, product requirements and agreed documentation scope.
Which records should a PCBA traceability plan include?+
Start with released files and revision, then define any required material or lot links, identifiers, process or inspection evidence, test results, disposition, retention and retrieval ownership. Only include records that are agreed for the project.
Who owns record retention?+
The product owner sets the required retention period and which records must be retrievable; the manufacturer stores and supplies the records it creates under the agreed order or quality terms. Name the system of record, unit or lot identifier, access method and handover format before the first build so a later failure can be traced without searching email attachments.
What changes require traceability review?+
Review the affected chain after a change to revision, BOM, approved alternate, supplier or consigned material, process route, identifier, test program, acceptance requirement or record-retention agreement.
Can X-ray and functional-test results be part of a traceability record?+
They can be included when the project scope defines the identifier, result format, acceptance basis and retention responsibility. Each result remains evidence for its stated inspection or test question only.
Technical references
Sources used for this guide
These sources explain the standards, materials or process details discussed above. Check the current revision when applying them to a new design.